ENGINEERING
Two Routes to One Chip: The Engineering Behind Kilby and Noyce
Kilby and Noyce made integration a practical design question. Their patents expose the roles of shared material, protected junctions and patterned connections.
Research checked
Newest cited publication
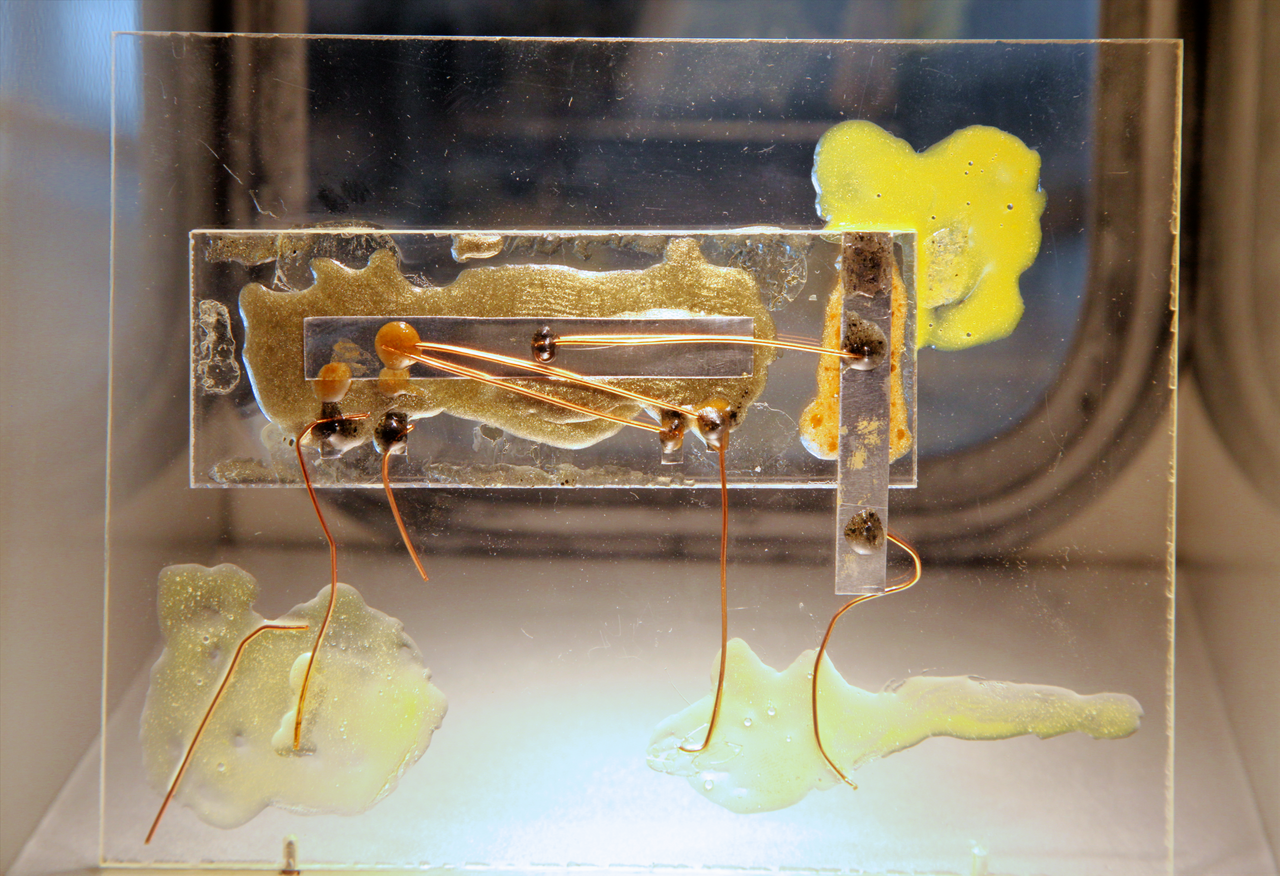
A museum replica of Jack Kilby’s first integrated circuit shows its semiconductor bar and connecting wires. The article also examines the distinct planar manufacturing approach associated with Robert Noyce.
Florian Schäffer / Wikimedia Commons · Image source · CC BY-SA 4.0

An electronic circuit needs both components and connections. Making its transistors smaller addresses only part of the problem if every connection still requires a separate assembly operation. The integrated-circuit inventions associated with Jack Kilby and Robert Noyce approached this larger problem through the semiconductor itself. Their patent documents, together with Jean Hoerni's manufacturing patent and Gordon Moore's early economic analysis, reveal complementary engineering questions: what can share a material, which regions must remain electrically separate, how can connections be made, and when does putting more functions together actually reduce cost?
Kilby made the whole circuit a material problem
Kilby's Miniaturized electronic circuits patent was filed on February 6, 1959, and published in June 1964. It proposes forming circuit elements within a semiconductor body using compatible processing steps. The document explicitly treats active and passive elements, including transistors, resistors and capacitors. It also discusses shaping the material and controlling current paths so that elements can perform distinct circuit functions. The underlying idea is broader than mounting separate miniature parts close together: the material and its geometry become the means of constructing the circuit.
That reframing creates a useful design exercise. Start with a circuit schematic and ask which properties each element needs: resistance, charge storage, rectification or amplification. Then ask whether those properties can be obtained through different regions of one physical structure. A line on the schematic that joins two symbols may become a shared region rather than an assembly joint. Conversely, two neighboring shapes may need deliberate electrical isolation. The mapping is therefore between functions and a manufacturable layout, rather than between a shopping list and a smaller container. It forces circuit design and fabrication to become parts of the same problem.
Hoerni made protection part of the process
Hoerni's Method of manufacturing semiconductor devices patent was filed in May 1959 and published in March 1962. It describes oxide layers used to define where diffusion occurs and to protect junctions, with openings made where contacts are required. The process retains protective material over sensitive junction boundaries rather than exposing the entire surface after forming the semiconductor regions. This is a manufacturing contribution with direct architectural consequences: a surface that can remain protected also provides a controlled foundation for further operations.
The important distinction is between a cover applied after a device is complete and a layer that helps determine how the device is made. Imagine a workshop jig that first locates a cut and then remains as a permanent protective part. Combining those jobs can remove a handling step, but only if the retained material remains compatible with later processing. For a semiconductor, compatibility includes electrical behavior, attachment to the surface and response to processing conditions. This reasoning does not imply that every protective layer is ideal. It shows why a successful manufacturing sequence can create design possibilities that a component-level schematic never explicitly requests.
Noyce addressed the connections above the silicon
Noyce's Semiconductor device-and-lead structure patent, filed in July 1959 and published in April 1961, describes metal strips extending across an insulating oxide layer. Selected openings permit electrical contact to semiconductor regions, while oxide insulates leads where they cross junction boundaries. The patent includes structures containing multiple circuit devices in one body. Its detailed discussion also recognizes unwanted capacitance between leads and underlying semiconductor. The connections become patterned features of the structure, with their own electrical consequences.
A connection is useful only if it reaches the intended region while avoiding unintended ones. Consider a road crossing several properties: the route, insulation and access points all matter, even when the destination is obvious. In an integrated layout, those choices can be specified geometrically and reproduced through shared fabrication steps. Yet replacing individual wires with patterned conductors does not abolish wiring problems. The designer still needs room to route signals, must prevent accidental contacts, and must account for interactions between nearby conductors. Integration changes the way those constraints are solved. It does not make the circuit an abstract diagram free from space and materials.
A small calculation explains the manufacturing incentive
Kilby's patent emphasizes how numerous separate fabrication and assembly operations can undermine an otherwise promising miniature circuit. To see the arithmetic without claiming historical production data, suppose a hypothetical assembly requires 100 independent operations, each succeeding with probability 0.999. The probability that every operation succeeds is 0.999 raised to the hundredth power, approximately 0.905. Under the same simplified assumptions, 1,000 operations yield approximately 0.368. A very good individual operation does not guarantee a high probability of a flawless large assembly.
This model deliberately assumes independent failures, identical operation quality and no repair. Real factories violate all three assumptions: one contamination event may affect multiple features, inspections may remove defects early, and rework may rescue some assemblies. The example therefore explains an incentive rather than predicting a factory's yield. Consolidating operations can help, but a shared process can also spread one failure across many elements. Engineers must measure the actual distribution of defects and identify correlated causes. Counting fewer assembly steps is useful evidence of a possible advantage; it is not, by itself, a complete reliability demonstration for the integrated product.
Moore's early question concerned an economic optimum
Moore's April 19, 1965 article, Cramming more components onto integrated circuits, describes a cost tradeoff. Adding components to a package could reduce cost per component, while declining yield could eventually reverse that benefit. He discussed the complexity associated with minimum component cost and projected its growth. The famous early forecast used an approximately annual doubling rate for the component count associated with minimum cost, an economic projection under stated manufacturing assumptions. His article also acknowledges limits for integrated inductors and large-value capacitors, whose functions require physical energy storage.
An engineer can restate the cost question with a deliberately simple model. Suppose a manufacturing run costs 1,000 units and produces 100 candidate chips. If half work, the manufacturing cost is 20 units per working chip before packaging and other costs. If a larger design produces only 40 candidates and half work, the comparable figure becomes 50 units. The larger chip may still be attractive if it replaces enough smaller chips and their surrounding connections. Economic integration therefore compares complete functions under stated assumptions. Neither the smallest chip nor the largest component count automatically wins that comparison.
Integration always leaves a boundary to engineer
Reading the four documents together suggests a more precise account of the landmark. Kilby's proposal treats multiple circuit functions as structures in semiconductor material. Hoerni develops protection and manufacturing control. Noyce describes patterned leads over an insulating surface. Moore asks how increasing complexity changes system economics. These roles overlap in their implications without being identical contributions. Patent filing and publication dates also answer different questions from dates of laboratory demonstrations; the records should not be collapsed into a single moment when every ingredient supposedly appeared fully formed.
A useful final design review asks what still crosses the package boundary: power, signals, heat and mechanical stress all require a path. Moving an amplifier onto a chip does not automatically integrate its power supply or eliminate the need to dissipate heat. Similarly, placing more circuit functions together may simplify assembly while making testing or replacement harder. The integrated circuit became a powerful engineering platform because functions, interfaces and fabrication could be reconsidered together. Its historical value is clearer when the remaining constraints stay visible: each successful integration redraws the boundary of the system, then gives engineers a new boundary to manage.
Sources & further reading
Primary papers, project documentation, and research releases used in this article. Publication dates below refer to the sources themselves.
- US3138743A: Miniaturized electronic circuitsJack S. Kilby / United States Patent Office, hosted by Google PatentsPublished Checked
- US3025589A: Method of manufacturing semiconductor devicesJean Hoerni / United States Patent Office, hosted by Google PatentsPublished Checked
- US2981877A: Semiconductor device-and-lead structureRobert N. Noyce / United States Patent Office, hosted by Google PatentsPublished Checked
- Cramming more components onto integrated circuitsGordon E. Moore / Electronics, archived by IntelPublished Checked
FOLLOW THE QUESTION
Explore engineering